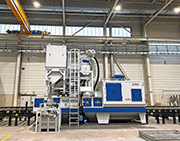
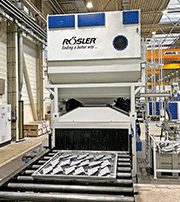
Flexible Roller Conveyor Shot Blast Machine Cleans Different Steel Plates and Fulfils Strict Maritime Quality Standards. The goal was maximum efficiency in all sectors. For this purpose, a German manufacturer of propulsion and maneuvering systems for ships and offshore installations modernized its manufacturing facilities. Part of the investment package was a roller conveyor blast machine, model RRB 22/5 from Rösler. This shot blast system, perfectly integrated into the overall manufacturing flow, allows partially automated cleaning of different flame-cut components and steel plates. To a large extent, it replaces manual shot blasting operations utilized to date.
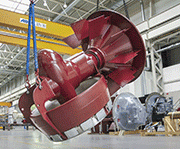
The invention of the controllable rudder propeller, horizontally movable by 360 degrees, in 1950 was the reason for the impressive success of SCHOTTEL GmbH. This innovation quickly transformed the company, founded in 1921, into a globally operating developer and manufacturer of maritime propulsion systems. With a portfolio of nine product types, offering a performance from 50 to 30,000 kW, the company offers by far the biggest range of ship and offshore propulsion and maneuvering systems in the world. In addition, the company offers comprehensive marine services such as intelligent remote access systems, data collection, data analysis, monitoring of the propulsion and maneuvering systems, and preventive maintenance. The products are made at two locations in Dörth and Wismar, both in Germany.
The combination of decades of experience in ship propulsion, modern hardware and software, and the latest scientific insights ensures that all products incorporate the latest technological developments and have excellent quality.
Automation, More Flexibility and High Equipment Uptimes Result in Significant Improvements in Operational Efficiency
To maintain its high technological standards, the company is constantly modernizing its manufacturing facilities. For example, the installation of a steel sheet line at the Dörth location made the manufacturing flow more efficient and more productive. This line includes the integration of an automatic steel sheet storage system, plasma/oxy-fuel flame cutting equipment, and switching the shot blast operation from a manual blast room to a continuous-flow mechanical blast machine. To minimize the personnel requirements and optimize internal logistics, the new roller conveyor blast machine was placed directly in line with the flame cutting equipment. A key customer requirement was that, after the blast operation, the steel surfaces must have a roughness depth of at least Rz = 70 µm. Under the highly corrosive maritime conditions, such roughness readings are essential to ensure the adhesive strength of the anti-corrosion paint applied during the subsequent paint operation.
To achieve the required surface roughness, SCHOTTEL used random-shaped abrasive blast media in its blast room. A key requirement for the new shot blast machine was that it must be able to handle a broad range of different workpiece sizes and guarantee a high uptime.
Clever Equipment Concept Offers High Performance and Operational Flexibility
During his search for a qualified shot blast equipment supplier, Frank Steinert, Manufacturing Manager at SCHOTTEL, contacted several companies, among them also Rösler Oberflächentechnik GmbH. This equipment manufacturer, located in Untermerzbach, developed a machine concept based on the standard roller conveyor machine RRB 22/5. The machine design was perfectly adapted to the customer requirements, which also include a special painting system. It allows shot blasting of steel plates up to five meters long, two meters wide, and 500 mm high. The roller conveyor, with a distance of 400 mm between rollers, allows blast cleaning of single steel components with a minimum length of 1,500 mm. A special transport frame allows safe processing of much smaller components.
Therefore, most of the flame-cut components, installed in the finished SCHOTTEL products, can now be manufactured much more efficiently. With the touch panel, the machine operator can easily select the respective shot blast programs from a program library stored in the machine controls.
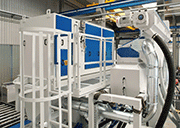
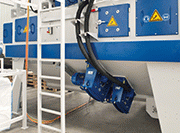
The blast machine is built from eight mm thick manganese steel. In addition, the blast room is lined with easily replaceable, overlapping wear plates made from the same wear-resistant material. Six high-performance Gamma 400G turbines – three blasting from the top and three from below – each with an installed power of 15 kW, ensure consistently high-quality shot blasting results. The Gamma turbines are equipped with Y-shaped throwing blades, which, compared to conventional turbines, produce 20% higher blast performance with, at the same time, lower energy consumption. The fact that both sides of the Y-shaped throwing blades can be used practically doubles their uptime. A quick-change system allows the replacement of worn blades with new ones without having to disassemble the turbine.
Another feature of the new system is that the dust collector was placed on the roof of the shot blast machine. This saved valuable manufacturing space. “We liked the equipment concept with its numerous technical features. However, before making our final decision, we wanted proof that all our requirements could be met,” comments Frank Steinert.
Shot Blasting Trials Under Actual Manufacturing Conditions
Shot blasting trials were made with a variety of typical SCHOTTEL workpieces. But in this case, they were not made at the Customer Experience Center of Rösler. Actually, the trials were conducted at a Rösler customer who has been using a nearly identical machine with the same turbine arrangement for the past three years. The blast trials proved not only that the specified shot blast results can be achieved consistently, but also that this is possible with a round, much less destructive, steel shot. The surface roughness values of the SCHOTTEL workpieces shot blasted with this customer’s machine were carefully evaluated. Frank Steinert explains: "To be absolutely sure, we subjected the test parts to paint adhesion and salt spray tests." An honest conversation with the reference customer regarding operational costs, wear characteristics, and time intervals between maintenance work was a decisive factor for choosing the RRB 22/5. "The results of the blast trials and the positive feedback from the reference customer absolutely convinced us that the RRB 22/5 meets all our quality demands and is therefore by far the best solution for us," concludes Frank Steinert.
Optimal Integration Facilitates Maintenance Work
Right from the beginning, the Rösler engineering team was participating in the planning activities at SCHOTTEL. Information about the available space at SCHOTTEL and suitable layouts greatly facilitated the perfect integration of the shot blast system into the building. This helped not only to simplify the concrete footing for the machine, but it also resulted in more space and comfort for the maintenance personnel.
For Information:
Rösler Oberflächentechnik GmbH
Vorstadt 1, 96190 Untermerzbach
Norman Peter, Germany
Tel. +49.9533.924-0
E-mail: n.peter@rosler.com
www.rosler.com

 BACK